2026 Best Way to Ensure Plastic Bottles Meet Global Standards

Time:2026-09-20 Author:Aria
0%

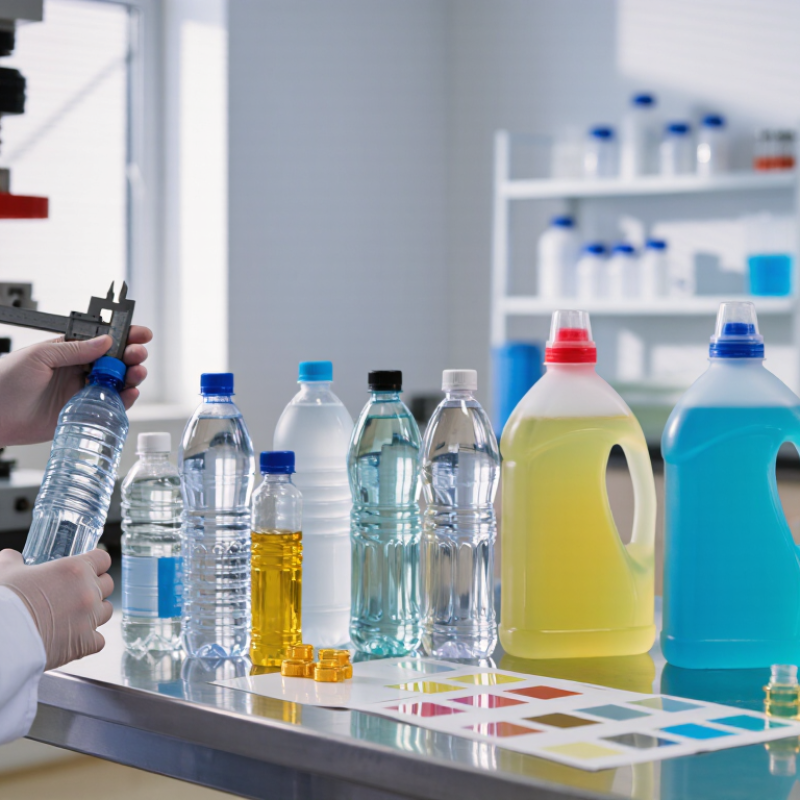
How to ensure plastic bottles meet international standards begins with one practical question: what will the bottle contain, and where will it be sold? A bottle for mineral water faces different risks than one for detergent or hot-fill juice. Manufacturers must identify the resin, additives, colorants, closures, and intended filling conditions. They should then compare requirements across major markets, including food-contact migration limits, material restrictions, labeling rules, and recycling obligations.

Testing must follow the product’s real journey. Samples should be exposed to heat, pressure, sunlight, cleaning chemicals, and repeated handling. Laboratories can check migration, leakage, torque, wall thickness, drop resistance, and seal performance. Batch records and resin certificates also matter. Without traceability, even an excellent test result may prove difficult to defend.

Dr. Jane Muncke, managing director of the Food Packaging Forum, has said, “Food packaging is a major source of human exposure to chemicals.” Her warning gives compliance a human meaning. A clear bottle on a production line is not automatically safe. It requires documented material selection and independent verification. Small defects matter.

This 2026 guide examines how to ensure plastic bottles meet international standards through risk assessment, supplier control, laboratory testing, and continuous production checks. It also considers ISO, ASTM, FDA, and European requirements without pretending they are identical. Standards change. Testing methods can differ. A careful manufacturer must review assumptions, not simply copy an old certificate. That step is often overlooked.
2026 Best Way to Ensure Plastic Bottles Meet Global Standards

Define Global Standards for Plastic Bottle Safety and Quality

Global plastic bottle safety begins with a clear definition of standards. A compliant bottle should protect water, resist leakage, and prevent harmful chemical migration. The WHO Guidelines for Drinking-water Quality provide the safety baseline for contents, while material rules such as EU Regulation 10/2011 and US 21 CFR requirements guide food-contact plastics. These systems assess substances, migration limits, manufacturing hygiene, and traceability. They are not identical. A supplier must compare requirements before selecting resin, additives, closures, and printing inks.

Industry data shows why this process matters. The OECD Global Plastics Outlook reports that only 9% of plastic waste was recycled globally in 2019. Recycled content needs careful testing, especially when bottles contact drinking water. UNEP’s 2023 report estimates that plastic pollution could fall by 80% by 2040 through better design, reuse, and recycling. That target is ambitious. It also exposes a weakness: recycled material claims can become vague without batch records and laboratory evidence.

Tips: Request migration-test reports, resin declarations, and lot-level traceability. Test bottles after heat, pressure, and transport simulation. Check odor and taste, too. A clean-looking bottle can still fail. Independent laboratories should verify results against the destination market’s rules. Review certificates annually, because suppliers, formulas, and regulations change. Some audits remain paperwork-heavy, so hands-on factory checks are still necessary.

Select Compliant Materials and Design Specifications

2026 Best Way to Ensure Plastic Bottles Meet Global Standards

Choosing compliant materials starts with the intended liquid, not the bottle’s appearance. A food-contact resin may still perform poorly with acidic drinks, oils, alcohol, or hot filling. Check supplier declarations, migration data, recycled-content controls, and batch traceability. Fit matters. Specify limits for heavy metals, additives, odor, and extractable substances according to each destination market. Do not treat one certificate as global approval. Requirements differ across jurisdictions and product categories.

Design specifications should convert compliance into measurable features. Define resin grade, wall thickness, neck finish, closure torque, thread profile, and tamper-evident performance. A 500-milliliter bottle needs stable dimensions, but lightweighting can create weak shoulder areas. Drop tests, top-load tests, leak tests, and pressure checks should represent real transport conditions. Use samples from early production, not only polished laboratory pieces. Small errors matter. A cap that feels secure may still leak after heat exposure or vibration.

Reliable verification combines documented drawings, controlled production records, and independent laboratory testing. Select laboratories with relevant accreditation and request methods, limits, and sample conditions in the report. Keep material lots linked to test results. This makes recalls and corrective actions more manageable. In practice, teams sometimes approve a beautiful prototype too early. That is a mistake worth admitting. Repeat testing after tooling changes, color adjustments, or recycled-content changes. Clear specifications protect performance, consumer safety, and market access without depending on a single document.

2026 Best Way to Ensure Plastic Bottles Meet Global Standards

Select recycled-content targets early and align bottle materials and specifications with the applicable market requirements.

The European Union requires 25% recycled plastic in PET beverage bottles from 2025 and 30% recycled plastic in all plastic beverage bottles from 2030. California requires 25% post-consumer recycled content in plastic beverage containers from 2025 and 50% from 2030. Actual compliance also depends on food-contact approval, migration testing, labeling, closures, and packaging design.

Control Manufacturing Processes and Testing Procedures

Plastic bottles meet global standards when control begins on the factory floor. Approved resin should arrive with traceable certificates and batch identification. Operators must check moisture, color, and contamination before production starts. A small moisture change can create weak walls, cloudy surfaces, or unstable dimensions.

Process control needs clear limits for temperature, pressure, cooling time, and cycle speed. Digital records help engineers identify drift before a full batch fails. Inspectors should measure bottle weight, neck size, wall thickness, and capacity at defined intervals. Keep samples from every production lot. They provide useful evidence during complaints or audits. Details matter.

Testing must reflect real handling conditions. Leak tests can reveal tiny seal defects that visual checks miss. Drop tests should use filled bottles and controlled heights. Compression testing shows whether containers survive stacking during transport. Migration testing should use suitable food-contact procedures and accredited laboratories. Equipment also needs scheduled calibration. However, records are not always perfect. A rushed inspection or unclear sample label can weaken confidence in otherwise good results. Teams should review these mistakes openly and improve the procedure, rather than hiding them. Personnel training, signed checklists, and independent verification make the system more reliable.

Verify Labeling, Traceability, and Documentation Requirements

2026 Best Way to Ensure Plastic Bottles Meet Global Standards

Clear labeling is the first control point. Each plastic bottle should show its material code, capacity, batch number, and responsible operator. Recycling instructions must match the actual resin, not a marketing assumption. A readable barcode or QR code should connect to production records, test results, and shipment details. It is not proof by itself. OECD’s Global Plastics Outlook reports that only 9% of plastic waste was recycled globally in 2019. Accurate labeling can support better sorting and accountability, although labels cannot repair poor waste systems.

Traceability should follow the bottle from resin receipt to filling, storage, and distribution. Record the supplier lot, machine line, production time, and inspection results. Keep these records consistent across paper and digital systems. Small mismatches matter. A missing batch code can delay a recall investigation. Documentation should include material specifications, food-contact declarations where relevant, migration testing, quality certificates, and change-control records. GS1 standards recommend structured identification for products and logistics units, making data easier to share across borders.

A practical audit should test one real bottle. Scan its code, open the linked record, and compare the resin, dimensions, and test date. Gaps often appear there. UNEP’s Turning off the Tap report says plastic pollution could be reduced by 80% by 2040 through system changes and better circularity. That target makes documentation more important, not less. Still, digital records can contain errors. Review them manually before shipment, especially after a supplier or label change.

Maintain Compliance Through Audits and Continuous Improvement

2026 Best Way to Ensure Plastic Bottles Meet Global Standards

Plastic bottle compliance depends on disciplined audits, not paperwork alone. The OECD Global Plastics Outlook reports that global plastic production reached 460 million tonnes in 2019. Packaging remains a major application, increasing pressure on manufacturers to prove material safety, strength, and traceability. A reliable audit should examine resin certificates, supplier changes, bottle dimensions, closure torque, leak resistance, and migration test results. Inspectors should also match production batches with laboratory records. Small gaps can become costly failures.

Make audits continuous and practical. Review incoming resin samples, check wall thickness at several points, and test filled bottles after transport simulation. Record calibration dates for scales, torque meters, and pressure equipment. The 2023 ISO Survey recorded more than 1.2 million ISO 9001 certificates worldwide, showing the value of structured quality systems. Certification alone is not enough. Corrective actions need an owner, deadline, evidence, and follow-up verification.

The uncomfortable truth is that one audit cannot expose every weakness. Sampling may miss a hidden variation. Operators may also follow procedures differently during busy shifts. Continuous improvement means studying complaints, near-misses, rejected batches, and supplier performance. Trends matter. A slightly rising leak rate deserves attention before it becomes a market issue. Review standards annually, train teams with real bottle defects, and challenge assumptions. Perfect compliance is difficult. Honest records make improvement possible.

2026 Best Way to Ensure Plastic Bottles Meet Global Standards - Maintain Compliance Through Audits and Continuous Improvement

Compliance Area Global Reference Requirement or Control Point Reference Value or Target Audit Evidence Recommended Review Frequency
Overall chemical migration European Commission Regulation (EU) No. 10/2011 Food-contact plastic materials must comply with applicable overall and specific migration limits under the intended conditions of use. Overall migration limit: 10 mg/dm² Accredited laboratory test report; material declaration; intended-use assessment Each new formulation and after a significant material or process change
Food-contact material safety Regulation (EC) No. 1935/2004 Materials must not transfer constituents to food in quantities that could endanger health, cause unacceptable changes, or impair taste or odour. Pass applicable migration and sensory requirements Compliance declaration; risk assessment; migration and organoleptic test records Before market entry and during periodic compliance reviews
Manufacturing hygiene and GMP Commission Regulation (EC) No. 2023/2006 Manufacturing processes must operate under documented good manufacturing practices with quality-assurance and quality-control systems. 100% of critical procedures documented and controlled Batch records; hygiene inspections; training records; deviation reports Internal audit at least annually; operational checks per shift or batch
United States food-contact compliance U.S. FDA 21 CFR Part 177 The polymer, additives, colorants, and processing aids must be permitted for the intended food-contact application and conditions of use. All constituents matched to applicable FDA provisions or authorization Supplier declarations; formulation review; FDA regulatory assessment; test reports At product development, supplier change, and regulatory update
Material traceability Regulation (EC) No. 1935/2004; ISO 22000:2018 principles Raw materials, production batches, processing records, and distribution information must be traceable through the supply chain. One-step-back and one-step-forward traceability Lot codes; purchase records; production logs; mock-recall results Traceability test at least annually and after system changes
Supplier qualification ISO 9001:2015 and ISO 22000:2018 control principles Suppliers of resin, additives, colorants, closures, and recycled content must be evaluated according to risk and approved before use. 100% of critical suppliers approved before purchase Supplier questionnaires; certificates; audit reports; incoming inspection data Annual review for critical suppliers; risk-based review for others
Recycled plastic content Applicable recycled-plastic legislation and destination-market rules Recycled material must be controlled for origin, contamination risk, process suitability, and documented use limitations. Documented recycled-content percentage and approved use Chain-of-custody records; decontamination validation; supplier declarations; test reports Each source change and periodic validation based on risk
Dimensional and functional quality ISO 9001:2015 quality-management principles Bottles should meet approved specifications for weight, capacity, neck finish, wall thickness, leakage resistance, and closure fit. Conformance to approved product specification First-article inspection; in-process measurements; leak tests; capability studies Start-up inspection and defined sampling during every production run
Nonconformity and corrective action ISO 9001:2015, Clause 10.2 Nonconforming product must be contained, investigated, corrected, and reviewed to prevent recurrence. 100% of critical nonconformities assigned an owner and due date Corrective-action records; root-cause analysis; effectiveness verification Immediate containment; effectiveness review after implementation
Internal audit program ISO 19011:2018 auditing guidance Audits should be planned using a risk-based program covering regulatory, material, process, hygiene, traceability, and product controls. All high-risk processes covered within the audit cycle Audit schedule; checklists; findings; corrective-action closure records At least annually, with increased frequency for high-risk processes
Continuous improvement ISO 9001:2015 improvement principles Audit findings, complaints, test failures, scrap, and process trends should be analyzed to prioritize measurable improvements. Quarterly review of compliance and quality trends Management-review minutes; KPI dashboard; improvement project records Monthly operational review and quarterly management review

Reference values and controls should be confirmed against the bottle material, food type, temperature, contact duration, recycled-content status, and destination-market requirements before release.

FAQS

What makes a plastic bottle suitable for drinking water?

It should protect the contents, resist leaks, and limit harmful chemical migration. Material safety is essential.

Which documents should suppliers provide?

Request migration-test reports, resin declarations, and lot-level traceability records. Match each report to its production batch.

Why are migration tests important?

Chemicals can move from plastic into water. Testing should consider heat, pressure, storage time, and transport conditions.

Should recycled plastic receive extra testing?

Yes. Recycled material may vary between batches. Verify its source, composition, cleaning process, and contact safety with laboratory evidence.

What should a factory audit inspect?

Check resin certificates, bottle dimensions, wall thickness, closure torque, leak resistance, and laboratory records. Small gaps matter.

Is certification alone enough?

No. Certification supports a quality system, but it cannot expose every hidden variation. Factory checks still matter.

How can teams find problems before complaints increase?

Track leaks, rejected batches, near-misses, and supplier changes. A slightly rising leak rate deserves attention.

How often should compliance records be reviewed?

Review them annually and after material, supplier, or regulatory changes. Records matter. Human review still has weaknesses.

What practical tests should filled bottles undergo?

Simulate heat, pressure, and transport. Check odor, taste, leakage, and bottle shape afterward. A clean-looking bottle can still fail.

How should corrective actions be managed?

Assign an owner and deadline, then record evidence and verify completion. Perfect compliance is difficult. Honest follow-up helps.

Conclusion

Ensuring plastic bottles meet global expectations requires a structured approach to safety, quality, and consistency. The first step is understanding the relevant international standards for materials, chemical safety, hygiene, strength, and product performance. Manufacturers should then select suitable, approved materials and establish design specifications based on the bottle’s intended use, capacity, closure system, and resistance requirements. Clear technical criteria help prevent defects and support reliable production.

How to ensure plastic bottles meet international standards also depends on disciplined manufacturing controls and thorough testing. Each stage should be monitored, from molding and cleaning to inspection and packaging, with tests covering dimensions, leakage, durability, and material safety. Accurate labeling, batch identification, traceability records, and complete compliance documentation are equally important. Regular internal audits, supplier reviews, corrective actions, and continuous improvement programs help maintain conformity over time and ensure that every production batch remains safe, consistent, and ready for responsible distribution across different markets.
Aria

Aria

Aria is a dedicated marketing professional with a deep passion for innovative strategies and a keen understanding of our company's product offerings. With a wealth of experience in the industry, Aria excels at crafting engaging content that highlights the unique features and benefits of our......